Raw Material Storage
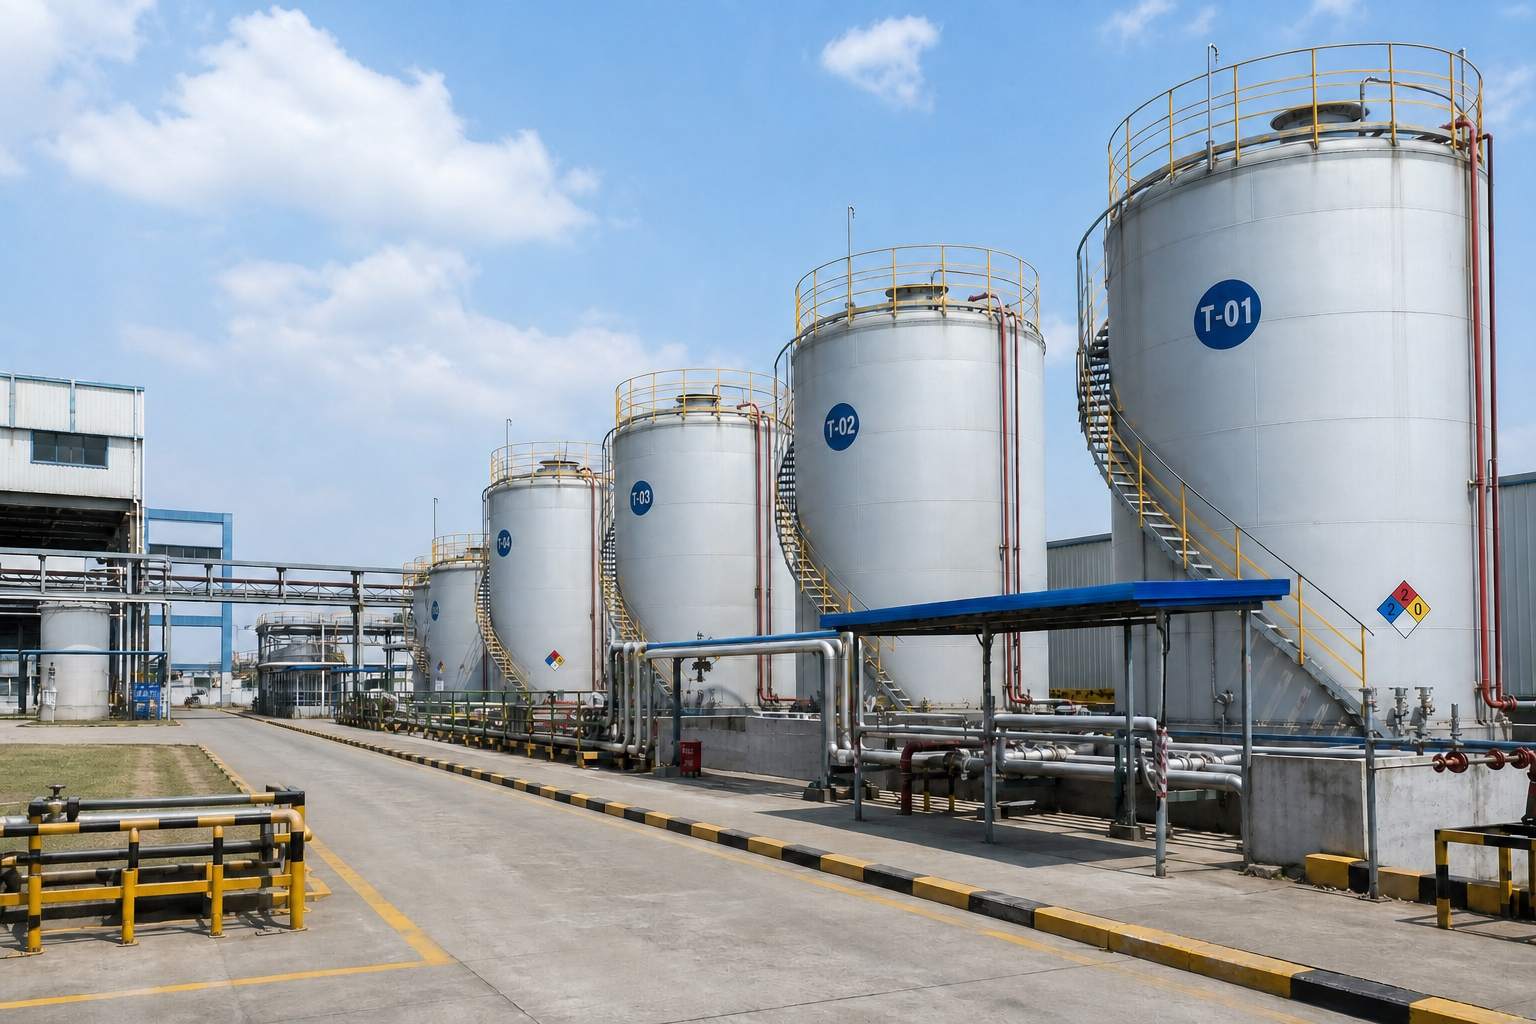
The raw material storage center is designed according to chemical storage regulations, implementing zoned and classified storage management. Raw materials of different properties are stored separately in dedicated warehouses, ensuring storage safety.
The warehouse is equipped with temperature and humidity real-time monitoring systems, 24-hour uninterrupted monitoring of environmental parameters. Once exceeding the set range, the system automatically alarms and starts adjustment equipment, ensuring raw material storage conditions are stable.
Incoming Inspection
All raw materials must undergo strict inspection before warehousing, including solvent purity, active ingredient content, propellant air tightness and other indicator tests. Unqualified raw materials are returned, ensuring product quality from the source.
Inventory Management
Using FIFO (First In First Out) management principle, ensuring raw materials are used within shelf life. The warehouse management system records in real-time each batch's warehousing time, inspection results, usage and other information, achieving full traceability.